

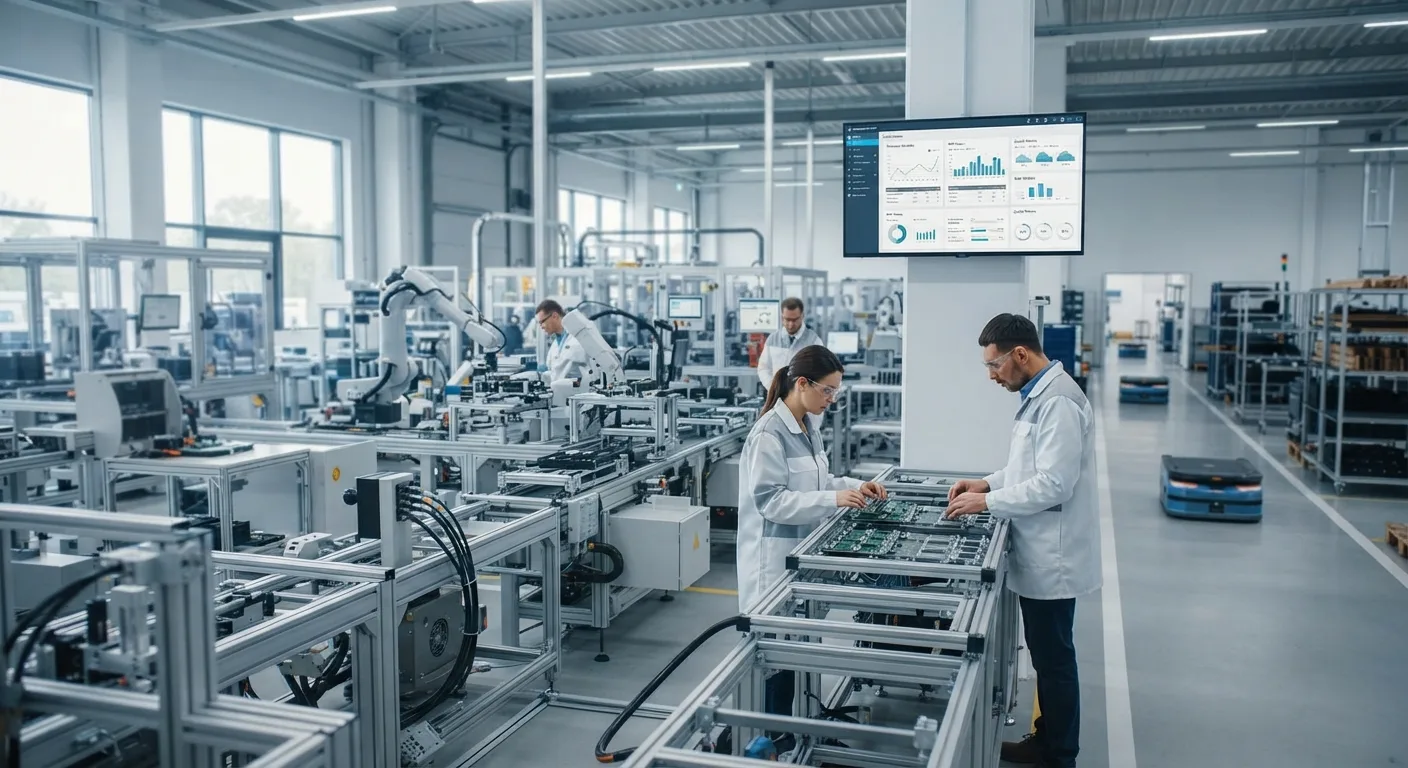
ERP in manufacturing isn’t limited to tracking inventory and accounting — it manages the entire production process in one system, from material requirements planning (MRP) to machine capacity, from quality control to costing. Rather than adapting a general-purpose ERP to manufacturing, choosing a system that includes manufacturing-specific modules from the start shortens implementation time and reduces operational errors. In this article, we cover the core components of manufacturing ERP.
What Is MRP (Material Requirements Planning)?
MRP (Material Requirements Planning) calculates when and how much of every raw material and sub-component needed to manufacture a product should be procured, based on the production plan. MRP automatically answers “which material should we order, and when?” by jointly evaluating the bill of materials (BOM), current stock levels, and lead time. A properly functioning MRP prevents both production stoppages caused by material bottlenecks and unnecessary excess stock.
Capacity Planning
Capacity planning calculates in advance whether existing machine and labor capacity can meet the planned production volume. While MRP answers “is there enough material?”, capacity planning answers “is there enough machine/labor time to process that material?” When the two don’t work together, the production line can hit a bottleneck even when materials are ready.
Quality Management Module
The quality management module in a manufacturing ERP defines quality control checkpoints at every stage from raw material intake to finished product, records defect/scrap rates, and provides lot-based traceability. When a quality issue is detected, it’s possible to trace back which lot, from which raw material, and on which shift it was produced — a mandatory requirement, particularly in regulated industries like food, pharmaceuticals, and automotive.
Comparing Manufacturing ERP Modules
| Module | Question It Answers | Risk If Not Used |
|---|---|---|
| MRP | Which material, when, how much to order? | Material bottlenecks or unnecessary excess stock |
| Capacity Planning | Is machine/labor capacity sufficient? | Delivery delays, idle capacity |
| Quality Management | Does the product meet standards, which lot is at fault? | Unable to trace the source during a recall |
| Costing | What is the real production cost of this product? | Incorrect pricing, hidden loss-making products |
Manufacturing ERP vs. General-Purpose ERP
Trying to bolt manufacturing modules onto a general-purpose ERP after the fact usually results in an incomplete or superficial solution. In an ERP designed specifically for manufacturing, MRP, capacity planning, and quality management work together from the ground up — a change in the bill of materials automatically flows through to material requirements, cost, and capacity calculations. This integration is one of the most critical criteria when manufacturing businesses choose an ERP.
Priority Order for SME-Scale Manufacturers
For a manufacturing SME with limited resources, rather than rolling out every module at once, starting with the area suffering the greatest losses (usually MRP, due to material bottlenecks) and gradually adding capacity planning and quality management both reduces risk and delivers an early return on investment.
Master Data Checklist Before Running MRP
MRP suggestions are only as accurate as the data behind them. Reviewing the points below before go-live prevents many of the incorrect order proposals seen in the first weeks.
- Bills of materials: Does every finished product have a current recipe with quantities and scrap rates?
- Stock records: Do system quantities match the results of a physical count?
- Lead times: Have realistic delivery times been entered for each supplier?
- Routings and work centres: Are operation times and machine definitions up to date?
- Units of measure: Are conversions between purchasing, stock and production units correct?
Doing this once is not enough. Decide early who approves changes to bills of materials and routings.
Common Mistakes in Manufacturing ERP Projects
Problems in production modules usually come from working habits rather than from the software. The most common mistakes are:
- Entering consumption and completed quantities in bulk at the end of the day. Stock looks wrong during the day and planning is misled.
- Defining safety stock and minimum order quantities once and never updating them.
- Closing production orders without recording scrap. Cost and quality reports no longer reflect reality.
- Planning in the system while the shop floor works from a separate Excel list.
- Leaving user training until the day of go-live.
All of these let system data drift away from the shop floor. Record transactions as they happen, by the person doing the work.
A Step-by-Step Approach to Go-Live
To limit risk, split the transition into small, measurable steps.
- Run a pilot with a single product group or production line.
- Initially, have a planner approve MRP suggestions before they become orders.
- Review deviations between planned and actual times, consumption and delivery dates every week.
- If a deviation is caused by a data error, correct the master data at its source, not the report.
- Once the pilot results are stable, add the other product groups one by one.
When planning these steps for your own production, ERP consulting can support you with process analysis and master data preparation.
Frequently Asked Questions
What’s the difference between MRP and MRP II?
MRP only plans material requirements, while MRP II (Manufacturing Resource Planning) is an expanded version that adds capacity, labor, and financial planning. Manufacturing modules in today’s ERP systems generally work on MRP II logic.
Does a small workshop need MRP?
Manual tracking quickly becomes complex as the variety of products and raw materials grows. Very small workshops working with few products/materials can get by with simple tracking, but as they grow, the need for MRP becomes unavoidable.
In which industries is a quality management module considered mandatory?
In industries like food, pharmaceuticals, cosmetics, and automotive, lot-based traceability is largely a legal requirement; in other industries it’s a voluntary but powerful quality assurance tool.
Conclusion
ERP in manufacturing doesn’t deliver full value without MRP, capacity planning, and quality management working together as one integrated system. Building these three components in an integrated way from the start directly improves both delivery performance and quality assurance. Get in touch to learn more about our ERP consulting service or to request a free quote for an ERP roadmap tailored to your manufacturing processes.
Want to bring your production process together in a single ERP system? Get in touch about our ERP consulting service or request a free quote.